

 English
 русский
 عربى
-
End Mill Chatter: Causes, Fixes, and How to Get Stable Milling Results
An end mill starts to scream after the first pass in a deep cavity. The surface looks like a washboard and the tool path no longer follows the programmed conto...
Industry News -
Driven Tools on CNC Roll Lathes: How to Choose, Size, and Justify the Payback
A nine-tonne work roll is sitting between centres, and the job sheet asks for a worn journal keyway to be re-cut plus four tapped holes on the end face. On a l...
Industry News -
CNC Machine Basic Knowledge: Axes, G-Code, Setup, and Safety for Beginners
A machinist loads a steel roll into a lathe, closes the guard, and presses cycle start. The turret indexes, the tool touches off, and the first pass cuts a cle...
Industry News -
CNC Lathe vs Milling: Key Differences and How to Choose the Right Machine
Which machine should you put on the floor when the new jobs include both shaft-like components and flat brackets? The answer is rarely black and white, but the...
Industry News -
The CNC Horizontal Lathe Buyer's Guide: Tips from a Roll Machine Builder
A roll shop supervisor once explained why the shop replaced its manual copying lathe for rough turning: the machine hit tolerance in the morning, but by the af...
Industry News -
CNC Feeds and Speeds Explained: The Machinist's Guide to Reliable Cutting
Feeds and speeds are not two separate numbers; they are a matched pair that control how a cutting tool engages the workpiece. Set them too low and the edge rub...
Industry News -
Climb Cutting vs Conventional Milling: How to Choose the Right Strategy
A typical CNC shop starts every new milling job with climb cutting, assuming it is always the best choice. Then a batch of hardened roller rolls arrives with a...
Industry News -
Climb Cutting vs. Conventional Cutting: When to Use Climb Milling in Production
Climb cutting delivers the cleanest, most accurate surface finish in CNC milling — but only when the machine and setup can handle the cutting forces. For rolle...
Industry News -
How to Operate a Lathe Safely: Step-by-Step Machine Setup and Turning Basics
Walk into any machine shop, and the lathe is the workhorse that turns raw bar stock into shafts, bushings, and precisely sized components. Yet the gap between ...
Industry News -
What Is a CNC Lathe Machine? Definition, Key Components, Types and Applications
A steel service center that needs 600 identical shafts, each turned to a diameter tolerance of ±0.01 mm, faces a straightforward decision: trust the judgment o...
Industry News -
How to Choose a Heavy Duty CNC Lathe: Specifications, Torque, and Rigidity
A production engineer evaluating a heavy duty CNC lathe usually has a concrete workload in mind: a 4,200 mm roll body to turn between centers, a 900 mm flange ...
Industry News -
CNC Lathe Maintenance: Daily, Weekly, and Annual Checklist for Reliable Machining
Midway through a production shift, a turning cell starts producing parts with a faint but measurable taper. Dimensions are still inside the tolerance band, but...
Industry News

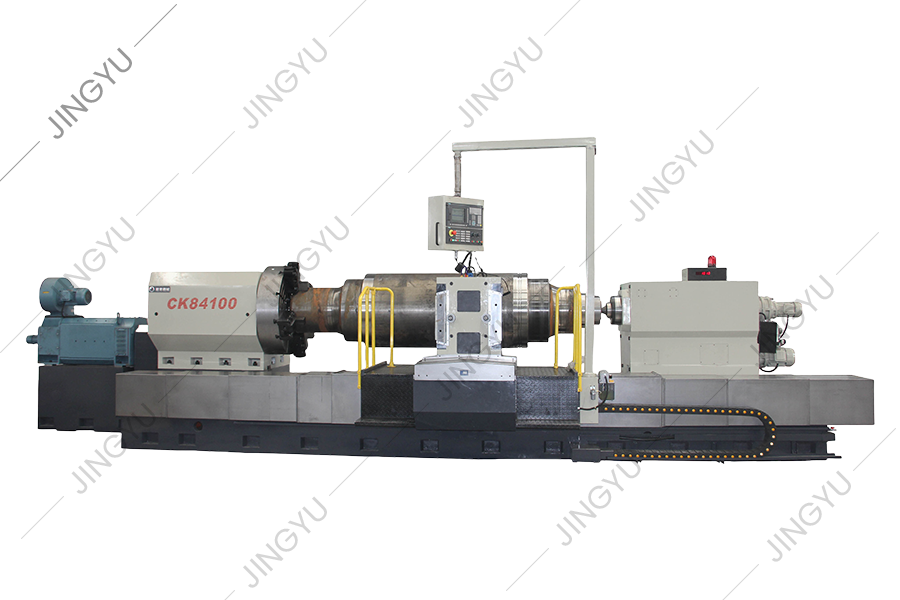
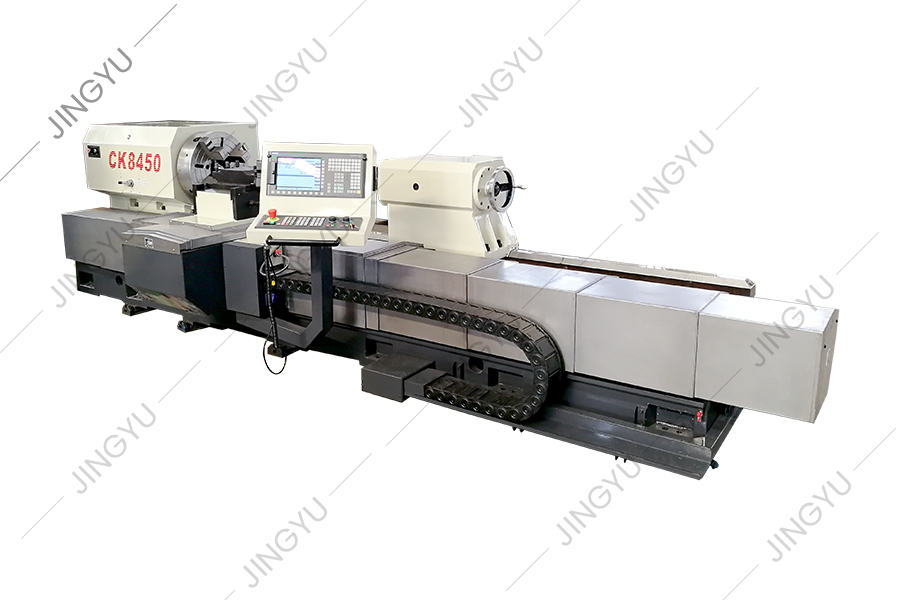
-
ADDRESS
No.3, Xinghe Road, Zhaxi Industrial Park, Chongchuan District, Nantong, Jiangsu Province, 226003, P.R.China
-
EMAIL
info@rolllathe.com jennifergao@rolllathe.com
-
PHONE
+86-513-85636116
Copyright © Nantong Jingyu Machinery Co., Ltd. All Rights Reserved
 China Roll Turning Lathe Manufacturers
